What is combustion control and O2 trim?
Combustion control is the system that sets fuel and air flow to a burner so it fires safely, cleanly and efficiently at every load. O2 trim is a closed-loop refinement of that control. An oxygen analyzer in the flue measures leftover oxygen, and the controller adjusts air to hold the right excess air level as conditions change.
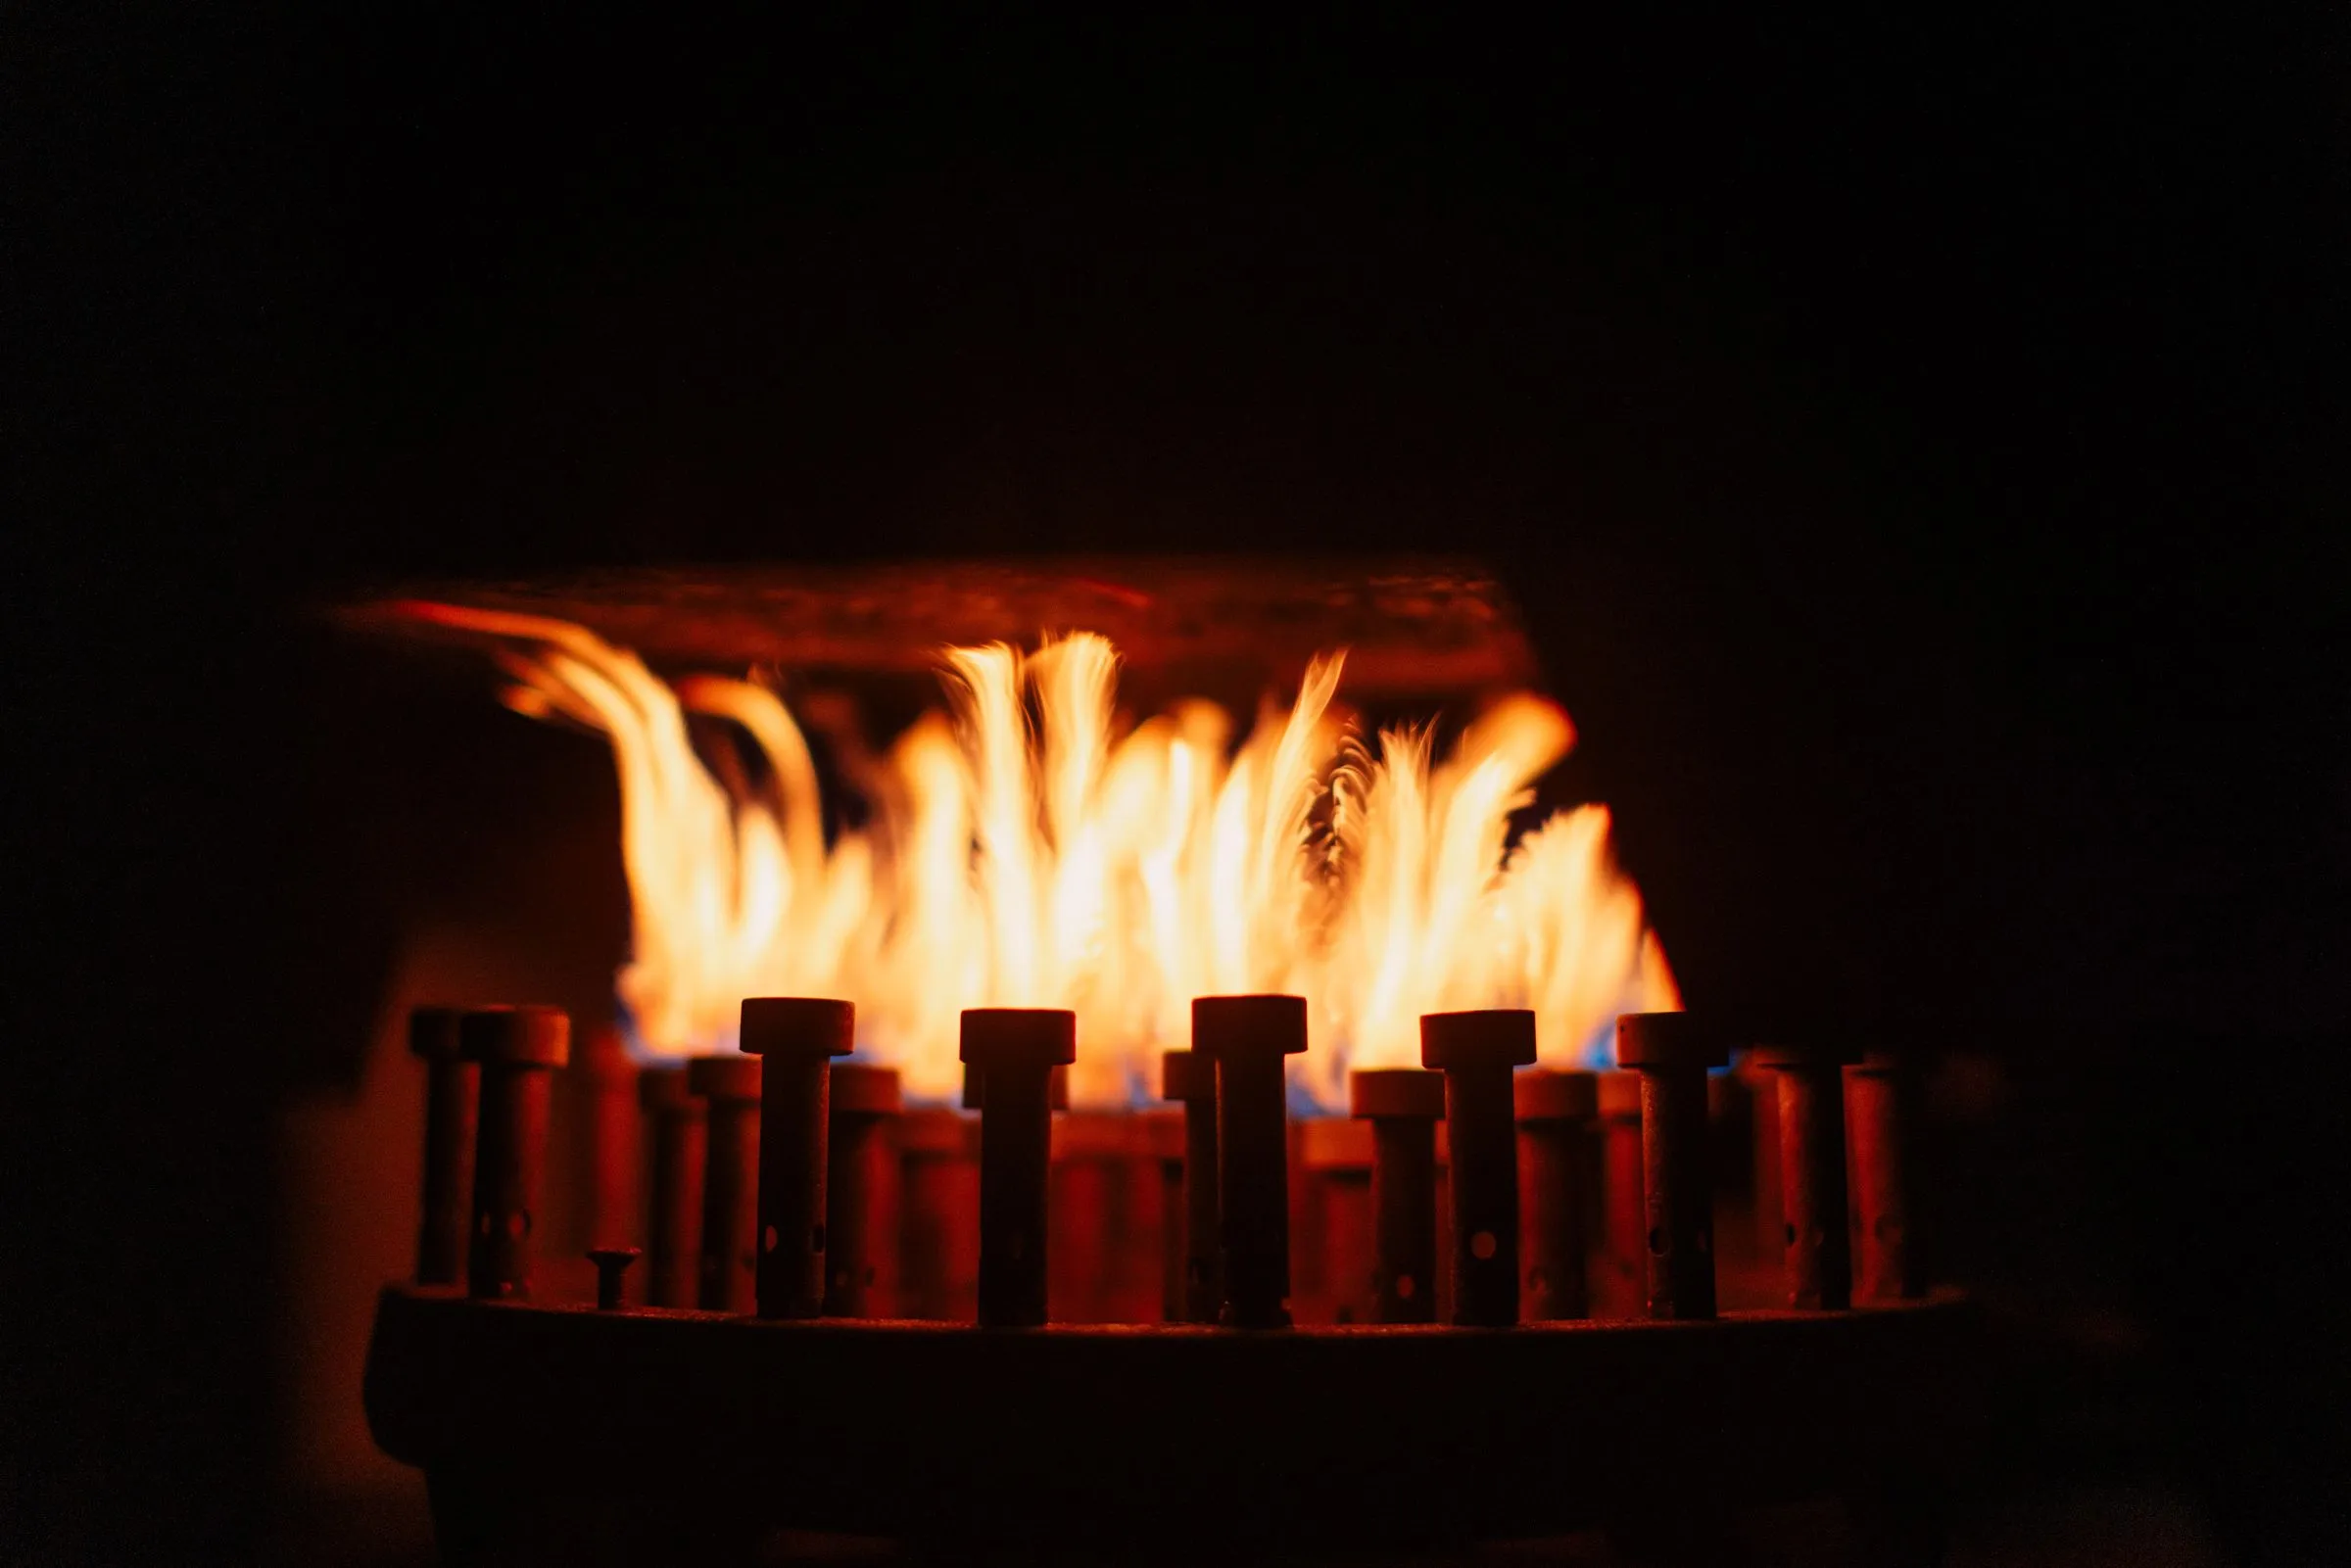
Every burner needs some excess air to burn fuel completely. Too little produces carbon monoxide, soot and unsafe conditions. Too much heats extra air that goes straight up the stack, wasting fuel. The goal of combustion control is to run consistently near the efficient middle, and the goal of burner management is to make sure that happens safely.
How combustion control technology works
Fuel/air ratio control. Older burners link the fuel valve and air damper mechanically through a jackshaft. Electronic ratio control, or parallel positioning, drives each with its own actuator along a programmed curve, with position feedback on every move.
Oxygen measurement. An in-situ zirconia probe sits directly in the flue gas. Heated zirconium dioxide conducts oxygen ions, and the O2 difference between flue gas and reference air produces a voltage the transmitter converts to percent oxygen. Measuring wet gas in place avoids sample lines and gives fast response.
Trim. The controller compares measured O2 with a load-dependent setpoint and corrects the air actuator or fan speed. LAMTEC’s adaptive CO/H2 control goes a step further, using a combination probe to find where unburned gases begin and running just on the safe side of that point.
Burner management and flame safety. Sequencing logic handles purge, ignition and flame proving. UV, IR or ionization scanners watch the flame continuously, and valve proving checks that safety shutoff valves seal.
| Control strategy | How air is set | Strength | Limitation |
|---|---|---|---|
| Mechanical jackshaft | Cams link fuel valve and air damper | Simple, low cost | Hysteresis, drift, no compensation |
| Electronic ratio control | Separate actuators follow programmed curves | Repeatable, multi-fuel capable | No correction for air density or fuel changes |
| O2 trim | Analyzer corrects air to an O2 setpoint | Compensates for ambient and fuel variation | Setpoint carries a safety margin |
| CO/H2 control | Trims toward onset of unburned gases | Lowest practical excess air | Requires combination probe and tuning |
Common applications
- Pulp and paper mills: power boilers, biomass and wood-waste combustion, and lime kilns across Alabama, Georgia, Mississippi and Louisiana.
- Gulf Coast refining and chemical plants: process heaters, steam boilers and thermal oil heaters, including hazardous-area installations.
- Food and beverage processing: steam boilers where fuel is a major operating cost.
- Power and utilities: utility boiler burners and multi-burner fireboxes.
- Industrial furnaces: thermal processing, glass and heat-treating furnaces.
Choosing the right combustion control solution
Start with the burner and its safety system, not the analyzer. A modern burner with electronic ratio control may need only an O2 probe and a trim function. An older burner with a mechanical linkage and aging flame safeguard often benefits more from a complete burner management upgrade that includes trim.
Code compliance comes next. NFPA 85, NFPA 86 or ASME CSD-1 may apply, along with insurer requirements and SIL targets from your hazard analysis. Finally, weigh integration and support: fieldbus connections to the DCS, commissioning, operator training and a local contact who understands the equipment.
Manufacturers we represent for combustion control
LAMTEC of Walldorf, Germany, specializes in combustion measurement and control. Its engineers brought O2 control to market in 1982 while part of ABB, and the company became independent in 1995. LAMTEC supplies the whole combustion loop, including the CMS and BurnerTronic BT300 burner management platforms, LT-series lambda transmitters and KS1D probes, F300K flame scanners, actuators, valves and pilot burners. Several devices carry SIL 3 certification, and key controllers hold UL and CSA approvals for North American projects. LAMTEC America in Hastings, Minnesota, supports the Americas.
Get local application support
Vaughn Associates can review your burners, flue gas measurement points and control architecture, and coordinate with LAMTEC America on scope and pricing. Visit engineering support, request a quote, or find your area manager on the territories page.